NEWS
21
Sep

Double Disc Grinding Wheels Deliver 0.002 mm Flatness on Valve Plates

Share:
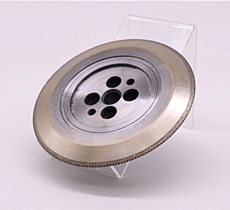
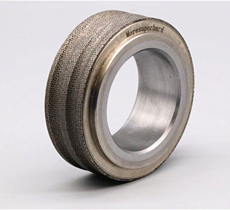
Valve plates are unforgiving components. Sealing surfaces must be flat, parallel and smooth enough that a hydraulic or compressor valve closes without leakage — batch after batch, thousands of parts at a time. Traditional single-side grinding struggles to hold those tolerances at production volume, and lapping adds cost and cycle time. That is why double disc grinding has become the standard route for valve plate finishing, and why wheel selection decides the entire process. This case study shows how MORESUPERHARD's double disc diamond/CBN grinding wheels performed on a LAPMASTER DSG720 machine, grinding CR2 steel valve plates to 0.002 mm flatness with cycle times under three minutes.


How Double Disc Grinding Works: Two Faces in One Pass


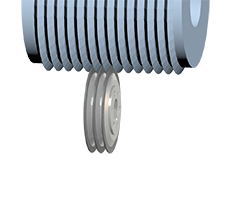
Double disc grinding machines hold a stack of workpieces in carriers between two opposing grinding wheels. Both faces are ground at the same time, in a single pass, so the relationship between the two faces — parallelism and thickness variation — is defined by the machine geometry rather than by two separate setups. This is the structural reason the process can hold sub-micron thickness control at production speed.
Compared with single-side grinding, double disc grinding removes the flip-and-relocate step that doubles cycle time and stacks up alignment error. Compared with lapping, it replaces a slow, consumable-heavy process with a fixed-abrasive wheel that wears predictably and dresses quickly. For flat parts like valve plates, connecting rods and gear plates, the double disc route is usually the fastest way to reach tight flatness and parallelism simultaneously — provided the wheels are matched correctly to the material and the machine.


The Challenge: Ultra-Tight Tolerances at Production Volume


In the precision manufacturing of critical components such as valve plates, three geometric targets dominate: flatness, parallelism and surface finish. Achieving them once in a toolroom is easy; holding them in high-volume production is where most processes break down. The customer in this case needed a wheel package that could:
  • Hold 0.002 mm flatness and sub-0.004 mm parallelism on every plate
  • Keep total thickness variation (TTV) below 0.001 mm
  • Remove 0.12-0.15 mm of stock per part without burning the surface
  • Finish each plate in under three minutes
  • Run reliably on an existing LAPMASTER DSG720 double disc grinder
Those are demanding numbers for any abrasive — especially with oil coolant and a relatively soft 20 HRC tool steel like CR2, which is prone to loading and heat marks if the wheel bond is wrong.


Case Overview: CR2 Steel Valve Plates on the LAPMASTER DSG720


The workpiece was a Ø120 mm valve plate machined from CR2 steel at 20 HRC, with casting as the pre-finishing process. Before finish grinding, the surface roughness stood at 6 RZ; the target after finish grinding was 3 RZ — with no burns and no burrs. MORESUPERHARD supplied double disc grinding wheels matched to the machine's spindle layout and the customer's oil coolant, then validated the package through production trials.
CR2 is a cold-work tool steel widely used for valve plates, dies and wear components. Its moderate hardness makes it machinable, but the combination of oil coolant and fine stock removal leaves little margin for a wheel that loads up or runs hot. Bond selection therefore focused on cool cutting with reliable chip clearance across the full 0.12-0.15 mm removal.


Key Process Parameters

 
Item Specification
Machine LAPMASTER DSG720
Spindle power Upper disc 5.5 kW / Lower disc 5.5 kW / Center 3 kW
Workpiece Valve plate
Material CR2 steel
Hardness 20 HRC
Workpiece size Ø120 mm
Coolant Oil
Stock removal 0.12 - 0.15 mm
Cycle time requirement < 3 minutes
Pre-finishing process Casting
Surface roughness before finish grinding 6 RZ
Surface roughness after finish grinding 3 RZ
Flatness after finish grinding 0.002 mm
Parallelism after finish grinding < 0.004 mm
TTV (total thickness variation) < 0.001 mm


Results That Speak for Themselves


The validated wheel package met every target in the trial protocol, and the production numbers tell a clear story:
  • Flatness of 0.002 mm — fully meeting the valve plate sealing requirement
  • Parallelism below 0.004 mm and TTV below 0.001 mm across the batch
  • Surface roughness improved from 6 RZ to 3 RZ in the finish pass, with no burns or burrs
  • Cycle time stayed under three minutes even while removing 0.12-0.15 mm of stock
  • Stable wheel wear behavior kept dressing intervals long and downtime low
For a valve plate line, that combination means more parts per shift, fewer rejections at final inspection and a process that does not need constant babysitting — the three things production managers actually measure.
The cost-per-part picture improved as well. Because the wheels held form over long intervals, dressing frequency stayed low, and the sub-three-minute cycle meant the machine's fixed hourly cost spread across more finished plates. When a wheel package both raises yield and shortens cycle time, the return on the wheel investment shows up in the same quarter.


Why Choose MORESUPERHARD Double Disc Wheels


Superior Precision

Flatness of 0.002 mm, parallelism under 0.004 mm and TTV under 0.001 mm are not laboratory numbers — they were sustained in production on CR2 steel, meeting the stringent demands of valve plate manufacturing.

High Productivity

The wheels consistently met the sub-three-minute cycle target even at full stock removal, boosting overall throughput without pushing the machine beyond its rated spindles.

Excellent Surface Quality

The finish pass brought roughness from 6 RZ down to 3 RZ with no burns and no burrs — critical for sealing surfaces where a single heat mark can leak.

Proven Compatibility

Wheels are available in resin or vitrified bond systems, optimized for oil coolant and materials like CR2 steel. Long wheel life reduces changeover downtime and cost per part.

Fully Customizable

Wheel dimensions, grit sizes and bond systems are tailored to your machine — LAPMASTER, Peter Wolters, Wendt, Diskus and other leading double disc grinders — instead of forcing your process into a catalog size.


Beyond Valve Plates: Where Double Disc Wheels Earn Their Keep


The same wheel technology transfers directly to any part that needs two parallel faces finished in one pass. Typical applications we supply include:
  • Connecting rods for automotive and compressor engines
  • Universal joints and drivetrain components
  • Hydraulic components: gear plates, spacers and manifolds
  • Bearings rings, seal rings and precision shims
In each case, MORESUPERHARD double disc grinding wheels provide a complete roughing-to-finishing solution that delivers higher precision, greater efficiency and lower overall cost per part.


Practical Tips for Stable Double Disc Grinding Results


Even the best wheel package only delivers its numbers when the surrounding process is disciplined. From our application experience across valve plate and hydraulic component lines, a few habits make the difference between holding tolerance shift after shift and drifting out of spec:
  • Keep coolant concentration and temperature stable; oil-based grinding is sensitive to viscosity changes that alter wheel loading
  • Filter coolant continuously; trapped swarf between wheel and workpiece is a leading cause of surface burns
  • Dress wheels on a fixed interval rather than waiting for finish to degrade, so the abrasive stays self-sharpening
  • Verify carrier thickness and slot condition regularly, since carriers that transmit uneven force create parallelism error
  • Log flatness and TTV per batch so trends are visible before they become rejects
When a customer buys a MORESUPERHARD double disc wheel package, these parameters come with it: recommended coolant, dressing schedule and starting feed values. The goal is that the first production run lands on target, not the fifth.


How to Specify Your Double Disc Wheels


When you request a quotation, share five things and our engineers will return a matched wheel recommendation:
  • Machine brand and model (e.g., LAPMASTER DSG720) and spindle power
  • Workpiece material, hardness and dimensions
  • Stock removal and cycle time targets
  • Coolant type (oil or emulsion)
  • Required flatness, parallelism and surface finish
With those inputs, we define grit size, bond system and wheel geometry so the first trial wheel is already close to production-ready.


Frequently Asked Questions


What flatness can double disc grinding achieve?
In this valve plate case, 0.002 mm flatness with TTV below 0.001 mm was sustained in production. Achievable tolerance depends on machine stiffness, material and wheel specification.
Which bond should I choose: resin or vitrified?
Both are available. Resin bonds suit many steel applications with oil coolant; vitrified bonds offer free-cutting behavior and easy dressing. Our engineers match the bond to your material and coolant.
Can wheels be made for my machine brand?
Yes. We manufacture to the mounting dimensions of LAPMASTER, Peter Wolters, Wendt, Diskus and other leading double disc grinders, with custom grit and bond options.
What materials work best?
Steels like CR2 at 20 HRC are well proven, and the range extends across cast iron, alloy steels and other ferrous alloys commonly used in hydraulic and automotive components.
How long does a custom double disc wheel order take?
Standard sizes ship quickly from stock; fully customized dimensions, grit and bond combinations typically run a few weeks from drawing approval. We confirm the exact lead time with every quotation.
Can we trial wheels on our own machine before committing?
Yes. We support trial runs: send your machine model, workpiece drawing and tolerance targets, and we will supply a trial wheel package with recommended parameters so you can validate results on your line.


Get Your Double Disc Wheel Package Quoted


If your valve plates, rods or hydraulic parts need tighter faces and faster cycles, send MORESUPERHARD your drawing and machine details. Our application team will propose the exact diamond or CBN double disc wheel package for your line — backed by a China manufacturer that exports worldwide.
 
Copyright © 2003-2023 More SuperHard Products Co., Ltd
Home
Whatsapp
E-mail
Inquiry