NEWS
05
Oct

Resin Diamond Grinding Wheels for Thermal Spray Coatings

Share:

The Thermal Spray Challenge: Hard Coatings That Are Hard to Grind


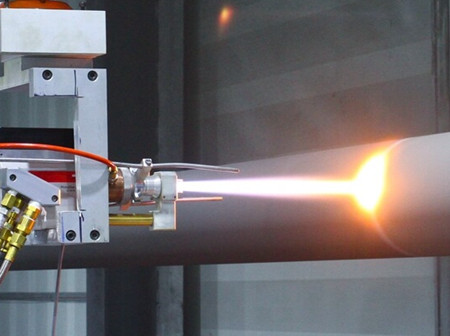
Thermal spray technology is a core process for industrial surface strengthening and restoration. Using flame, plasma, or high-velocity oxy-fuel (HVOF) methods, hard powders such as tungsten carbide, chromium carbide, and chromium oxide are sprayed onto workpiece surfaces to form protective coatings that are extremely hard, wear-resistant, and corrosion-resistant. These coatings are widely used on metallurgical rolls, wind-power main shafts, aerospace components, and construction machinery parts.

                        Resin Diamond Grinding Wheels for Thermal Spray Coatings


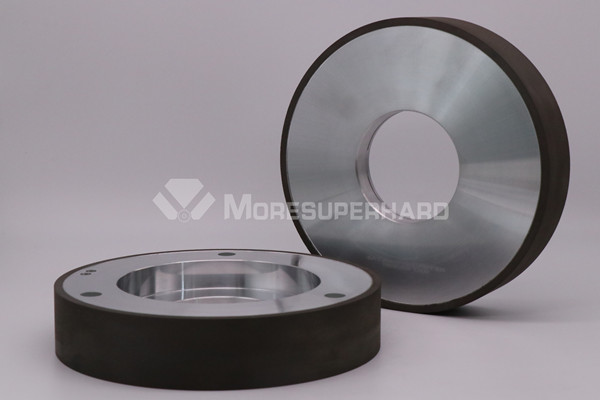
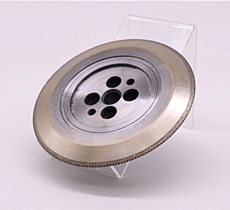
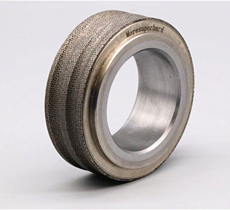
But thermal spray coatings create a serious grinding problem. They are hard, dense, rough, and bonded to a complex substrate interface—so conventional wheels often cause coating chipping, grinding burn, poor flatness, and rapid tool wear. The solution: a resin-bond diamond wheel sized specifically for large sprayed components—750 × 80 × 305 mm with 120/140 grit—engineered to finish thermal spray coatings reliably and economically.


Key Specifications for Large Thermal Spray Workpieces


The wheel is manufactured to standard industrial precision dimensions, fully compatible with large external and surface grinding machines:
  • Geometry: 750 mm outer diameter × 80 mm height × 305 mm bore. The large diameter suits big roll-grinding machines, covering a large surface area per pass for large shafts and sprayed parts. The thick 80 mm abrasive layer provides high rigidity, preventing vibration and deformation during grinding and ensuring uniform processing of large surfaces. The 305 mm bore is standard and fits most machine spindles without modification.
  • Grit size: 120/140. This medium-fine grit is the sweet spot for finishing thermal spray coatings—it combines high productivity with precision, reduces the risk of scratching and coating chipping compared with coarse grits, and lowers cutting resistance and heat build-up compared with very fine grits. It suits semi-finishing and finishing of sprayed coatings.
  • Bond: special high-temperature resin bond. The formulation is optimized for the intense heat generated when grinding high-hardness coatings. It offers toughness, excellent self-sharpening, and thermal stability—it will not soften or shed grains under heat, so the wheel stays sharp, while the resin cushions impact loads and protects brittle sprayed coatings from peeling and chipping.


Four Key Advantages: Solving the Industry’s Grinding Pain Points


                  https://www.mogrinding.com/products/grinding-wheels/resin-diamond-cbn-wheel/diamond-cylindrical-wheel-for-thermal-spraying-coated.html


Thermal spray coatings—carbide and ceramic composites—are far harder than ordinary steel, brittle, and often uneven in thickness. That demands exceptional sharpness, stability, wear resistance, and temperature control from the grinding tool. The resin diamond wheel delivers on all four:
  1. Stable grinding of high-hardness coatings: Diamond abrasive is far harder than corundum or silicon carbide, so it machines tungsten carbide, chromium carbide, and chromium oxide coatings easily. Abrasive wear is minimal, wheel life is long, tool-change frequency drops, and abrasive costs fall. The tough resin bond absorbs grinding shocks, preventing coating delamination and micro-cracks while preserving the protective properties of the sprayed layer.
  2. Excellent self-sharpening, no workpiece burn: Overheating is the biggest danger in sprayed-coating grinding—it oxidizes the coating and softens the base metal. The resin bond self-sharpens continuously: dulled grains break away to expose fresh sharp edges, reducing grinding resistance and heat generation. The wheel’s open pore structure provides efficient heat dissipation and chip removal, preventing workpiece burn, coating discoloration, and thermal deformation.
  3. High finishing accuracy, excellent surface quality: The 120/140 grit combined with precision manufacturing produces a flat working surface with evenly distributed diamond grains. Finished parts achieve stable surface roughness and meet assembly requirements immediately, without extra polishing. The rigid 750×80×305 design runs without runout at high speed, holding accuracy along the full length of large parts.
  4. Wide application range, high cost-performance: The wheel suits coatings produced by HVOF, plasma, arc, and flame spraying, and covers metallurgy, wind power, petrochemical, aerospace, and heavy machinery workpieces. Compared with ceramic-bond and metal-bond diamond wheels, the resin wheel delivers better surface finish, gentler coating protection, and a more attractive price—ideal for serial industrial production.


Applications in the Thermal Spray Industry


Thanks to its large size and 120/140 grit, this wheel is designed for finishing sprayed coatings on large components:
  • Finishing large rolls after spraying: Metallurgical, paper, and textile rolls with sprayed tungsten-carbide coatings need roundness, cylindricity, and surface roughness corrected. The wheel suits external roll-grinding machines, delivering uniform large-area processing and the required surface accuracy.
  • Large wind-power and petrochemical components: Wind-turbine shafts, hydraulic piston rods, and wear-resistant pipeline parts are cleaned of spray particles and flattened after coating. The 120/140 grit balances productivity and surface quality for high-precision assembly.
  • Brittle ceramic and carbide coatings: For fragile chromium oxide and chromium carbide coatings, the resin wheel’s gentle grinding action avoids chipping, holds layer thickness precisely, and finishes the part while preserving its protective properties.


Practical Value and Usage Recommendations


Coating grinding is the final operation that determines the quality of sprayed parts. Conventional abrasives are slow, generate high scrap rates, and wear out quickly on hard sprayed layers. The 750×80×305 resin diamond wheel at 120/140 grit raises precision and productivity on large parts, cuts scrap from coating damage, reduces machine downtime for tool changes, and lowers production costs.
For best results, use a precision large CNC grinding machine, select feed and speed carefully, and avoid overloaded dry grinding. Coolant improves heat removal and chip evacuation, further improving surface quality and extending wheel life.


Conclusion: The Preferred Wheel for Large Sprayed Workpieces


The tailored dimensions, thermal-spray-specific bond formulation, and balanced efficiency-versus-precision performance make the 750×80×305 mm resin diamond wheel at 120/140 grit the preferred abrasive for finishing large components with thermal spray coatings. Its stable grinding behavior and excellent final quality match the industry’s drive toward higher precision, higher efficiency, lower cost, and greater process stability—supporting the upgrade of surface strengthening and restoration processes for industrial parts.


Why Choose Our Resin Diamond Wheels for Thermal Spray


                       Resin Diamond Grinding Wheels for Thermal Spray Coatings


We engineer resin-bond diamond grinding wheels specifically for thermal spray coatings—including large formats such as 750 × 80 × 305 mm in 120/140 grit and other custom sizes. Our wheels are manufactured with precisely controlled diamond concentration, grit, and high-temperature resin bond formulation, delivering stable material removal, burn-free surfaces, and long service life on tungsten carbide, chromium carbide, and chromium oxide coatings. We offer full customization of diameter, width, bore, grit, and bond to match your roll grinders and sprayed workpieces, plus application engineering support for feed, speed, and coolant optimization. Contact us today with your coating type, workpiece size, and current process—we will build the right thermal spray grinding solution for you.


Frequently Asked Questions


Q: What grinding wheel should I use for thermal spray coatings?
A: Use a diamond wheel—diamond is far harder than corundum or silicon carbide, so it machines tungsten carbide, chromium carbide, and chromium oxide coatings efficiently. For large sprayed workpieces, a resin-bond wheel such as 750 × 80 × 305 mm at 120/140 grit provides stable, burn-free finishing with long life.

Q: Why choose a resin bond over ceramic or metal bond for sprayed coatings?
A: Resin bond self-sharpens continuously, preventing heat build-up and workpiece burn, and cushions impact loads to protect brittle coatings from chipping. It also delivers better surface finish and lower cost than ceramic or metal bonds—ideal for finishing hard, brittle sprayed layers.

Q: What grit is best for finishing thermal spray coatings?
A: 120/140 grit is the recommended sweet spot for semi-finishing and finishing sprayed coatings. It combines high removal with precision, avoids scratching and chipping (unlike coarse grits), and limits cutting resistance and heat (unlike very fine grits).

Q: Why do thermal spray coatings burn during grinding?

A: Sprayed coatings are hard and dense, generating intense heat at the contact zone. Without self-sharpening abrasive and good heat dissipation, the surface overheats, oxidizing the coating and softening the base metal. Resin-bond diamond wheels with open pore structure remove heat and chips fast, preventing burn.

Q: Can one wheel grind HVOF, plasma, arc, and flame spray coatings?

A: Yes. Resin-bond diamond wheels suit coatings produced by HVOF, plasma, arc, and flame spraying across metallurgy, wind power, petrochemical, aerospace, and heavy machinery applications, as long as the wheel size and grit match the workpiece and machine.

Q: How should I use a large resin diamond wheel for sprayed rolls?

A: Mount it on a precision large CNC roll grinder, select feed and speed for the coating, avoid overloaded dry grinding, and use coolant to improve heat removal and chip evacuation. This extends wheel life and maximizes surface quality.
 
FOLLOW US
This Blog keeps our valued customers informed of important Radiac News and Events, and in the industries we serve.
Copyright © 2003-2023 More SuperHard Products Co., Ltd
Home
Whatsapp
E-mail
Inquiry